

Rare Earth Ore Powder Pneumatic Conveying: A Solution for Material Transport Beyond Distance Limits
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional engineering firm based in Shandong, China. The company specializes in the design, manufacturing, and installation of advanced material handling systems, particularly focusing on pneumatic conveying solutions for challenging applications such as rare earth ore powder transport.

Rare Earth Ore Powder Pneumatic Conveying System
Our core product, the rare earth ore powder pneumatic conveying system, addresses the critical need for efficient and reliable material transport in industrial settings. This technology enables the movement of fine powders like rare earth ore over extended distances without the limitations of traditional methods. The system utilizes air as the conveying medium, ensuring a clean, dust-free, and low-maintenance operation that minimizes product contamination and environmental impact.

Key Advantages of Pneumatic Conveying for Rare Earth Powders
One of the primary benefits of our pneumatic conveying solution is its ability to overcome distance barriers. Unlike mechanical conveyors that are often constrained by layout and infrastructure, pneumatic systems can transport materials over several kilometers with consistent performance. This flexibility is particularly valuable in mining and processing facilities where the ore extraction and processing plants may be located far apart. Additionally, the system offers superior control over the flow rate and pressure, allowing for precise regulation of the material transport process. This precision is essential for maintaining the quality and integrity of rare earth powders, which are sensitive to handling conditions.
Application in Rare Earth Processing
In the rare earth ore processing industry, the efficient transport of fine powders from crushers, classifiers, and storage silos to processing units is crucial for maintaining production efficiency. Our pneumatic conveying system provides a seamless solution for this challenge. By eliminating the need for multiple transfer points and mechanical components, the system reduces downtime and maintenance costs. The air-based transport also prevents the buildup of dust and debris, which can affect the purity of the rare earth materials. This ensures that the final products meet the stringent quality standards required by the electronics and manufacturing sectors.
System Components and Operation
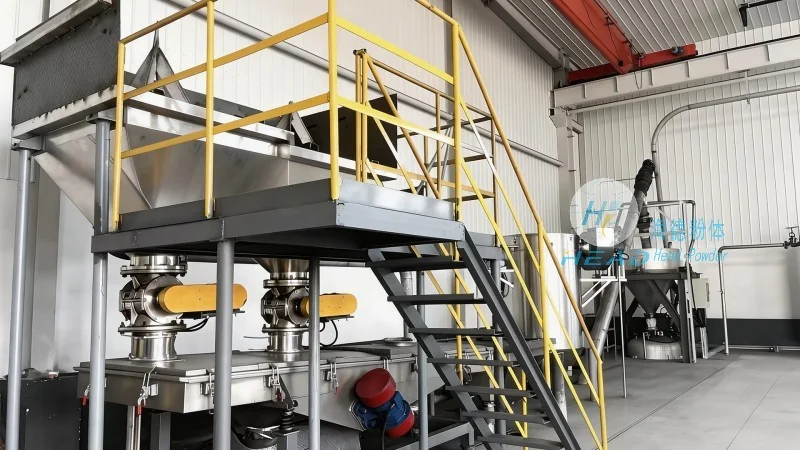
The rare earth ore powder pneumatic conveying system consists of several key components, including a feed hopper, a rotary airlock valve, a conveying line, and a receiver tank. The process begins with the material being fed into the hopper from the source. The rotary airlock valve then regulates the flow of the powder into the conveying line, where it is mixed with compressed air. The air-powder mixture travels through the pipeline under pressure, reaching the receiver tank at the destination. The air is then separated from the powder in the receiver, and the powder is discharged for further processing. This closed-loop system ensures minimal product loss and environmental contamination.

Conclusion and Commitment
Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative and reliable material handling solutions for the rare earth industry. Our pneumatic conveying system for rare earth ore powders offers a cost-effective and efficient alternative to traditional transport methods, enabling businesses to overcome distance limitations and improve overall operational performance. With our expertise in engineering and manufacturing, we deliver customized solutions that meet the specific needs of each client, ensuring long-term success and sustainability in material transport.