

Introduction to Barley Pneumatic Conveying Systems: Structure and Working Principles
HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems tailored for agricultural applications, particularly for barley handling. The company's expertise lies in creating efficient and reliable systems that ensure the safe and efficient transport of barley from storage to processing facilities.

Overview of Barley Pneumatic Conveying Systems
A pneumatic conveying system for barley is a mechanized solution that uses air pressure to move grain through a network of pipes. This method offers significant advantages over traditional mechanical conveyors, such as reduced labor costs, minimized product damage, and enhanced hygiene. The system typically consists of several key components, including a hopper for material storage, a blower or compressor to generate airflow, a conveying line with appropriate fittings, and a separation unit to collect the material at the destination.
Structural Components and Working Principles
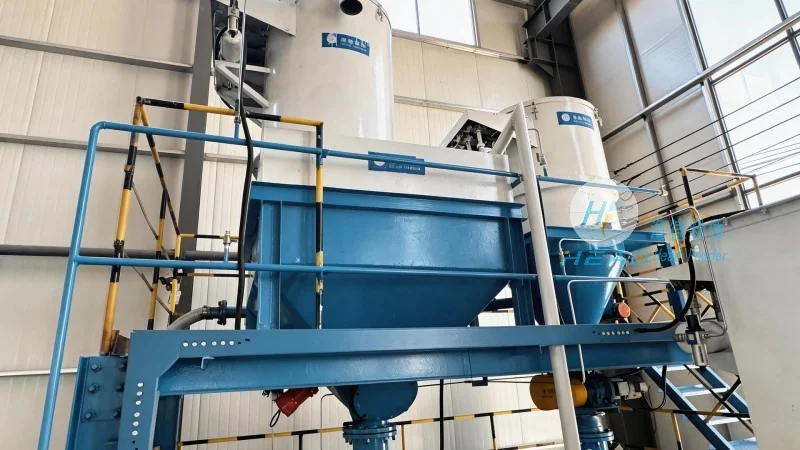
The core structure of a barley pneumatic conveying system is designed to handle the unique characteristics of barley, such as its size, density, and susceptibility to breakage. The system's components work in a coordinated manner to ensure smooth material flow. For instance, the hopper is equipped with a discharge valve that controls the flow rate of barley into the system. The blower, often a positive displacement type, generates the necessary air pressure to propel the barley through the pipeline. The conveying line is made of durable materials like stainless steel or PVC to withstand the abrasive nature of the grain and prevent clogging.
Key Functional Elements and Their Roles
Several functional elements are integral to the operation of the barley pneumatic conveying system. The airlock or rotary valve at the inlet of the hopper prevents backflow and maintains consistent material feed. The filter system is crucial for maintaining air quality and preventing dust from entering the blower, which can cause damage and reduce efficiency. The separation unit, such as a cyclone or bag filter, collects the barley at the end of the conveying line and returns it to the process or storage area. This unit also helps in capturing any fine particles that may have escaped, ensuring a clean and efficient operation.
Advantages of Using Pneumatic Conveying for Barley Handling
Implementing a pneumatic conveying system for barley offers numerous benefits. Firstly, it provides a dust-free environment, which is essential for maintaining product quality and worker safety. Secondly, the system minimizes product breakage, preserving the integrity of the barley grains, which is vital for milling and brewing applications. Thirdly, the automated nature of the system reduces labor requirements and increases operational efficiency. Additionally, the system's flexibility allows for easy integration with existing processing lines, making it a cost-effective solution for both new and existing facilities.

Customization and Application Scope
HeadPowder Engineering Co., Ltd. offers customized solutions to meet the specific needs of barley handling operations. The company's engineers work closely with clients to design systems that match their production capacity, space constraints, and budget. The systems can be tailored for various applications, including transporting barley from silos to milling machines, moving grain between storage and processing units, or even for bulk handling in large-scale agricultural operations. The company's commitment to quality and innovation ensures that each system is built to withstand the demands of continuous operation and provides long-term reliability.
Conclusion and Company Commitment
In conclusion, the barley pneumatic conveying system is a sophisticated and efficient solution for handling barley in agricultural and food processing industries. With its ability to maintain product quality, reduce labor costs, and enhance operational safety, it has become a preferred choice for many facilities. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to lead in the development of advanced pneumatic conveying systems, providing tailored solutions that meet the evolving needs of the barley processing sector. The company's dedication to quality, innovation, and customer satisfaction ensures that clients receive systems that are not only efficient but also durable and reliable for long-term use.