

What is a Bulk Material Storage and Powder Handling System? Explained Design Principles
Bulk material storage and powder handling systems are critical components in various industrial applications, designed to efficiently store, transport, and manage bulk materials such as powders, granules, and other particulate substances. These systems play a vital role in ensuring smooth operations across sectors like pharmaceuticals, food processing, chemical manufacturing, and more. Understanding the core components and design principles of such systems is essential for optimizing material flow and maintaining operational efficiency.

Key Components of a Bulk Material Storage System
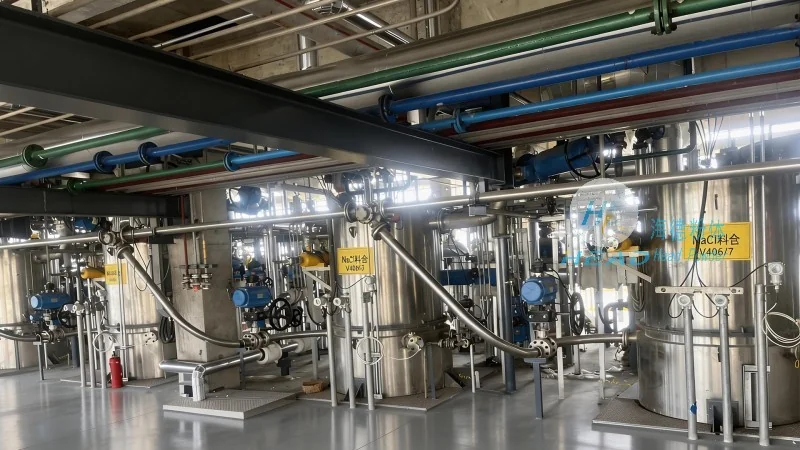
The foundation of any effective bulk material storage system lies in its key components, which work in harmony to facilitate material handling. The primary elements include bulk storage silos or hoppers, which are engineered to hold large volumes of material under controlled conditions. These structures are typically made from durable materials like steel or reinforced concrete, ensuring longevity and resistance to corrosion and wear. Additionally, aeration systems are often integrated to prevent material caking or compaction, maintaining material flowability. Level sensors and monitoring devices are crucial for real-time tracking of material levels, enabling automated control and preventing overfilling or underfilling.

Design Principles for Efficient Powder Handling
The design of a powder handling system revolves around several fundamental principles aimed at maximizing efficiency and minimizing operational risks. One of the core principles is the consideration of material properties, including particle size, density, and flow characteristics. This information is critical for selecting appropriate equipment, such as conveyor systems or pneumatic conveyors, that can handle the specific material without causing degradation or blockages. Another key principle is the implementation of airtight and sealed systems to prevent contamination and dust emissions, which is particularly important in industries like pharmaceuticals and food processing. The design also emphasizes energy efficiency, with features like variable speed drives and optimized airflow to reduce operational costs while maintaining performance.

Role of HeadPowder in Providing Advanced Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing and supplying high-quality bulk material storage and powder handling systems. With a strong commitment to innovation and customer satisfaction, HeadPowder leverages advanced engineering techniques to design systems tailored to the unique needs of each client. The company’s expertise spans the entire lifecycle of a system, from initial design and customization to installation and maintenance. By focusing on material-specific solutions, HeadPowder ensures that its systems not only meet but exceed industry standards, providing reliable and efficient performance in demanding environments.
Applications and Industries Served
Bulk material storage and powder handling systems are widely used across diverse industries, each with specific requirements. In the pharmaceutical industry, these systems are essential for maintaining the purity and integrity of raw materials and finished products. The food processing sector relies on them to handle ingredients like flour, sugar, and spices, ensuring consistent quality and preventing contamination. Chemical manufacturers use such systems for handling reactive powders and granules, where safety and material control are paramount. Additionally, in the agricultural and mining sectors, these systems facilitate the storage and transport of bulk commodities, improving logistics and reducing handling costs.
Conclusion: Enhancing Operational Efficiency with Professional Systems
Investing in a well-designed bulk material storage and powder handling system is a strategic decision that can significantly enhance operational efficiency and reduce costs in various industrial settings. By understanding the key components and design principles, businesses can select the most suitable system for their needs. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing tailored solutions that address specific material challenges and industry requirements. As industries continue to evolve, the importance of reliable and efficient powder handling systems remains paramount, ensuring smooth material flow and maintaining competitive advantages.