

Working Principle and Features of Coal Ash Powder Pneumatic Conveying Equipment
Coal ash, a byproduct of coal combustion in thermal power plants, requires efficient and reliable handling to ensure environmental compliance and resource utilization. Pneumatic conveying systems have emerged as a preferred solution for transporting coal ash powder due to their ability to handle fine particulate materials with minimal dust generation and operational flexibility. This article delves into the working principle and key features of coal ash powder pneumatic conveying equipment, highlighting how such systems enhance industrial efficiency and sustainability.

Working Principle of Coal Ash Powder Pneumatic Conveying Equipment
The core mechanism of coal ash powder pneumatic conveying equipment revolves around the use of compressed air or other gas streams to transport solid particles. In a typical system, the coal ash powder is introduced into a hopper or feeder, where it is then drawn into a pipeline by the moving air. The air velocity within the pipeline is maintained above the minimum fluidization velocity of the coal ash particles, ensuring that the particles remain suspended and transported as a homogeneous mixture. This process, known as dilute-phase pneumatic conveying, is characterized by high flow rates and low pressure drops, making it suitable for long-distance and high-capacity applications. The system typically includes components such as a blower or compressor to generate the necessary air pressure, a hopper for material storage, a feeder to control the flow rate, and a pipeline network to direct the material to its destination. The air and solid mixture is then separated at the receiving end, often through a cyclone or filter, where the coal ash is collected and the air is either recirculated or vented. This separation process is critical for maintaining the purity of the transported material and preventing dust contamination in the environment.
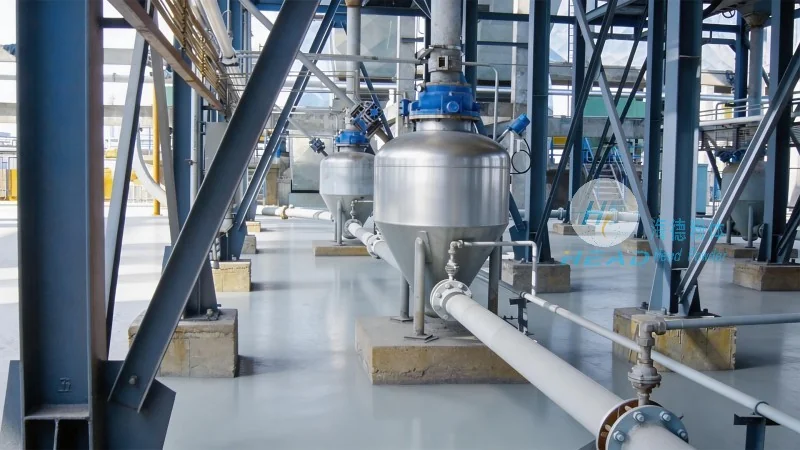
Key Features of Coal Ash Powder Pneumatic Conveying Equipment
Coal ash powder pneumatic conveying equipment offers several advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and enclosed transport solution, which is essential for environmental protection and worker safety. Unlike traditional belt or bucket elevators, pneumatic systems minimize the release of fine particles into the air, reducing the risk of respiratory issues and environmental pollution. Secondly, the equipment is highly efficient in terms of material handling, capable of transporting large volumes of coal ash over long distances with minimal energy consumption. The use of compressed air allows for precise control over the flow rate and pressure, ensuring consistent and reliable operation. Thirdly, the system is versatile and adaptable to various coal ash characteristics, including different particle sizes, moisture contents, and bulk densities. This flexibility allows manufacturers to customize the equipment to meet specific operational requirements, such as handling high-temperature or abrasive coal ash. Additionally, the equipment is relatively compact and easy to install, making it suitable for both new and retrofit applications in power plants and industrial facilities. The low maintenance requirements and long service life of pneumatic conveying systems further contribute to their cost-effectiveness, as they require fewer moving parts and less frequent repairs compared to mechanical conveying systems.

Applications and Benefits in Industrial Settings
Coal ash powder pneumatic conveying equipment is widely used in thermal power plants, cement factories, and other industrial facilities that generate large quantities of coal ash. In power plants, the equipment is employed to transport coal ash from the boiler to storage silos or disposal sites, ensuring that the ash is handled safely and efficiently. The enclosed system prevents ash from being released into the atmosphere, which is crucial for meeting environmental regulations and maintaining air quality. In cement plants, coal ash is often used as a supplementary cementitious material, and pneumatic conveying systems facilitate the transport of ash from storage to the cement production line. This not only improves the efficiency of the cement manufacturing process but also reduces the reliance on natural raw materials. The benefits of using such equipment extend beyond environmental and operational aspects. For instance, the reduced dust generation leads to lower cleaning costs and improved workplace conditions. Moreover, the ability to handle abrasive coal ash without significant wear and tear on components makes the equipment durable and long-lasting. The overall impact of these features is a significant reduction in operational costs and an enhancement of the plant's sustainability profile.

Manufacturer and Company Background
HeadPowder, a leading manufacturer of industrial conveying equipment, specializes in the design and production of coal ash powder pneumatic conveying systems. With a strong presence in the industry, HeadPowder has established itself as a trusted provider of high-quality equipment tailored to the needs of power plants and industrial clients. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing technologies and a team of experienced engineers to develop innovative solutions. HeadPowder's commitment to quality and customer satisfaction is reflected in its adherence to international standards and rigorous testing protocols. The company's products are designed to meet the specific requirements of coal ash handling, ensuring optimal performance and reliability. By partnering with HeadPowder, industrial facilities can benefit from cutting-edge technology and expert support, enabling them to enhance their operational efficiency and environmental performance.