

Operation Process and Working Principle of Gray Bin Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems. The gray bin material handling system is a critical component in various industrial applications, offering efficient and reliable solutions for bulk material transport. This system is engineered to meet the demands of modern manufacturing and processing industries, ensuring seamless material flow from storage to processing units.

System Overview and Key Components
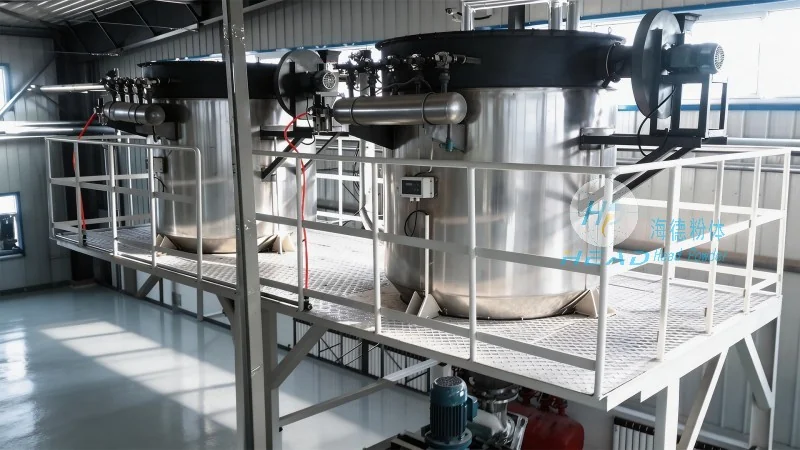
The gray bin material handling system typically consists of several integrated components that work in harmony to facilitate material transport. The primary elements include the gray storage bins, conveyor mechanisms, control systems, and feeding devices. Each component is meticulously designed to optimize performance and durability. The gray bins are constructed from high-quality materials, providing robust storage capabilities for various bulk materials such as powders, granules, and other granular substances. The conveyor systems, which may include belt conveyors, screw conveyors, or pneumatic conveyors, are tailored to the specific material characteristics and operational requirements.
Operation Process of the Material Handling System
The operation of the gray bin material handling system follows a systematic sequence to ensure efficient material transport. Initially, materials are loaded into the gray storage bins, either manually or through automated feeding mechanisms. Once the bins are filled, the control system activates the conveyor system, initiating the material transport process. The conveyor mechanisms then move the material from the storage bin to the processing or packaging stations. The system may include multiple bins and conveyors, allowing for continuous operation and reduced downtime. The control system monitors the entire process, adjusting the speed and direction of the conveyors as needed to maintain optimal material flow. This sequential operation ensures that materials are transported safely and efficiently, minimizing the risk of spills or blockages.
Working Principle of the Material Handling System
The working principle of the gray bin material handling system is based on mechanical and pneumatic principles, depending on the specific design. For systems utilizing belt conveyors, the material is transferred through the movement of a continuous belt, which is driven by a motor. The belt moves at a controlled speed, carrying the material from the storage bin to the next stage of processing. Screw conveyors operate by rotating a screw within a tube, pushing the material forward through the system. Pneumatic conveyors, on the other hand, use compressed air to transport the material in a sealed pipe, which is particularly effective for handling fine powders and granules. The control system plays a crucial role in regulating the flow rate and pressure, ensuring that the material is transported without clogging or loss. This integrated approach to material handling ensures that the system operates reliably and consistently, meeting the performance standards of industrial applications.

Technical Advantages and Applications
The gray bin material handling system offers several technical advantages that make it suitable for a wide range of industrial applications. Its robust construction and durable materials ensure long-term performance and minimal maintenance requirements. The system's flexibility allows for customization to accommodate different material types and processing needs. Additionally, the integrated control system provides real-time monitoring and adjustment capabilities, enhancing operational efficiency. The system is widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining, where efficient material transport is critical to production processes. By optimizing material flow, the system reduces labor costs, minimizes material loss, and improves overall productivity.