

What is a Mineral Sand Powder Conveyor? And What Are Its Design Principles?
Mineral sand powder conveyors are specialized equipment designed to transport bulk materials such as mineral sands, powders, and granules in industrial settings. These systems are crucial for efficient material handling in mining, processing, and manufacturing operations. Understanding the function and design principles of such conveyors is essential for optimizing production processes and ensuring safety and reliability in material transport.

Introduction to Mineral Sand Powder Conveyors
A mineral sand powder conveyor, also known as a bulk material conveyor, is a mechanical system used to move loose, granular, or powdery materials from one location to another. These conveyors are widely used in industries like mining, chemical processing, and food production where the handling of mineral sands and other fine materials is required. The primary goal of these systems is to achieve efficient, continuous, and controlled movement of materials without degradation or loss.
Key Components of a Mineral Sand Powder Conveyor
Headpowder, a leading manufacturer based in Shandong, China, designs and manufactures high-quality mineral sand powder conveyors. The core components of these systems typically include a drive system, a conveyor belt or screw mechanism, a hopper or feeding device, and a control system. The drive system provides the necessary power to move the material, while the conveyor mechanism (either a belt, screw, or pneumatic system) transports the material along the designated path. The feeding device ensures a consistent flow of material into the conveyor, and the control system monitors and adjusts the operation for optimal performance.

Design Principles for Efficient Material Transport
The design of a mineral sand powder conveyor is tailored to the specific characteristics of the material being transported, including particle size, density, and flowability. Key design principles include ensuring minimal material degradation, preventing blockages or clogging, and maintaining consistent material flow. For example, the conveyor belt material is often selected based on the abrasiveness of the mineral sand to prevent wear and tear. Additionally, the inclination angle of the conveyor is carefully calculated to balance the material's natural angle of repose with the required transport speed, ensuring efficient movement without excessive energy consumption.
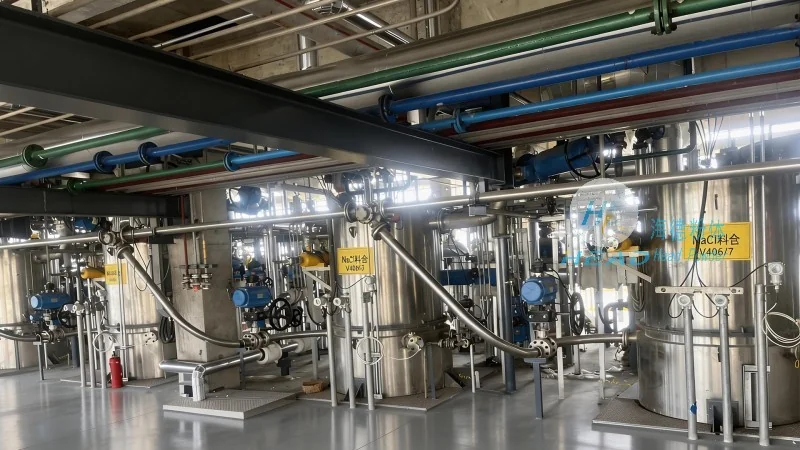
Advantages of Using a Mineral Sand Powder Conveyor
Implementing a mineral sand powder conveyor offers several advantages for industrial operations. Firstly, these systems provide a continuous and automated material transport solution, reducing the need for manual handling and associated labor costs. Secondly, they enhance safety by minimizing the risk of dust exposure and material spills, which are common in traditional manual handling methods. Thirdly, the controlled environment of the conveyor system helps maintain the quality of the mineral sand, preventing contamination or degradation during transport. Finally, the energy efficiency of modern conveyor designs reduces operational costs while maintaining high throughput rates.

Application Examples in Industrial Settings
Headpowder's mineral sand powder conveyors are used in a variety of industrial applications. In mining operations, these systems transport crushed mineral sands from processing plants to storage facilities or for further processing. In chemical plants, they handle fine powders and granules during the production of minerals and chemicals. Additionally, in food processing industries, they are used to transport ingredients like flour or sugar while maintaining hygiene standards. The versatility of these conveyors makes them suitable for a wide range of applications where efficient bulk material handling is critical.
Conclusion and Company Overview
Mineral sand powder conveyors are essential equipment for modern industrial operations, providing efficient and reliable transport of bulk materials. The design principles and components of these systems are carefully engineered to meet the specific needs of each application, ensuring optimal performance and durability. Headpowder Engineering Co., Ltd., with its headquarters in Shandong, China, specializes in the design and manufacturing of high-quality mineral sand powder conveyors, offering tailored solutions to meet the diverse needs of industrial clients. By leveraging advanced engineering and materials, Headpowder ensures that its conveyors deliver consistent performance and contribute to the overall efficiency of material handling processes.