

Principle and Working Scene Characteristics of Bentonite Powder Pneumatic Conveying Machines
Bentonite powder, a versatile and essential material used in industries ranging from mining and construction to chemical processing and food production, demands efficient and reliable handling solutions. The pneumatic conveying machine emerges as a sophisticated solution, leveraging air pressure to transport dry powders through a sealed pipeline system. This article delves into the operational principles of these machines and outlines their key working scene characteristics, offering a comprehensive understanding of how they optimize material handling in industrial settings.

Principle of Operation
The fundamental principle of a bentonite powder pneumatic conveying machine revolves around the creation of an air-driven flow that entrains and transports powder particles. The system typically comprises a hopper for material storage, a high-pressure blower or compressor to generate airflow, and a network of pipelines that guide the material from the source to the destination. As the air moves through the pipeline, it creates a suction effect that pulls the bentonite powder particles into the stream, forming a cohesive mixture. This process eliminates the need for mechanical components like conveyor belts or screw conveyors, reducing friction and wear on the equipment. The machine operates by maintaining a consistent pressure differential between the inlet and outlet, ensuring smooth and continuous material flow. The design allows for flexible pipeline routing, enabling the system to adapt to complex plant layouts and production requirements. The enclosed nature of the system also minimizes dust emissions and prevents product contamination, making it suitable for applications where hygiene and purity are critical.
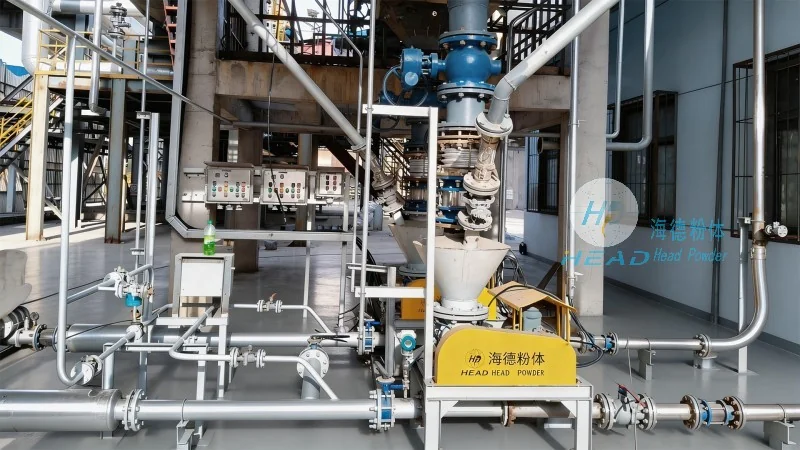
Working Scene Characteristics
The working scene characteristics of bentonite powder pneumatic conveying machines are tailored to meet the diverse demands of industrial environments. These machines are commonly deployed in scenarios such as mining operations, where large volumes of bentonite are extracted and transported to processing facilities. In chemical plants, they facilitate the transfer of fine powders between reactors and storage tanks, ensuring precise dosing and reducing material loss. The food industry also utilizes these systems for handling ingredients like bentonite in food processing, where maintaining product quality and safety is paramount. The key characteristics include high efficiency in material transport, with the ability to handle large volumes at a consistent rate. The enclosed system design enhances safety by preventing dust dispersion and reducing the risk of fire or explosion in areas where powders are handled. Additionally, the machines are designed for low maintenance, with components that are easy to replace and inspect, minimizing downtime and operational costs. The working scene also highlights the adaptability of the pneumatic system, which can be integrated with other equipment like mixers or classifiers, creating a seamless material handling workflow. The flexibility in pipeline routing allows for easy expansion or reconfiguration of the system as production needs evolve, making it a long-term investment for industrial operations.

Company Overview
HeadPowder, a prominent player in the material handling equipment industry, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, combines decades of experience with cutting-edge technology to deliver high-performance solutions for bentonite powder handling. The company’s commitment to innovation is evident in its product development, which focuses on enhancing efficiency, safety, and reliability. HeadPowder’s team of engineers and technicians works closely with clients to understand their specific requirements, ensuring that each pneumatic conveying system is customized to meet operational needs. The company adheres to stringent quality standards, with all products undergoing rigorous testing and certification before deployment. By leveraging its expertise in pneumatic technology, HeadPowder provides comprehensive solutions that improve production efficiency and reduce operational costs for industrial clients. The company’s presence in Shandong, China, allows it to serve a wide range of domestic and international markets, reinforcing its position as a trusted partner in the industry.