

Principle and Working Scene Characteristics of Manganese Carbonate Powder Conveying System
For industries dealing with manganese carbonate powders, efficient and reliable powder conveying systems are crucial for maintaining production efficiency and product quality. Manganese carbonate, a key raw material in various industrial applications, requires specialized handling due to its fine particle size and potential for dust generation. The Manganese Carbonate Powder Conveying System developed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges through a combination of advanced technology and robust design, ensuring safe and effective material transport in industrial settings.

Core Principles of the Conveying System
The fundamental principle of the Manganese Carbonate Powder Conveying System is to transport fine powders like manganese carbonate from storage to processing equipment or packaging areas with minimal loss, contamination, and energy consumption. The system typically integrates components such as feeders, conveyors (e.g., pneumatic or mechanical), dust collection systems, and control units to achieve seamless material flow. The design emphasizes low air velocity to prevent particle segregation and high efficiency to reduce operational costs, making it suitable for both small-scale and large-scale production environments.
System Components and Their Functions
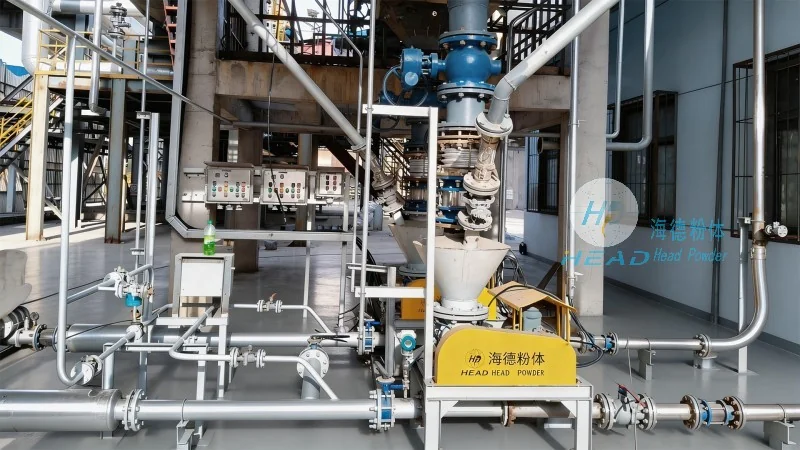
The Manganese Carbonate Powder Conveying System consists of several key components, each playing a vital role in the overall operation. The feed hopper is responsible for storing and feeding the powder into the system, ensuring a consistent material supply. The feeder, often a rotary or vibratory type, controls the flow rate of the powder, preventing overloading or underfeeding that could disrupt the conveying process. The conveyor itself, which may be pneumatic (using air to transport particles) or mechanical (using belts or screws), moves the powder through the system. Pneumatic conveyors are particularly effective for fine powders as they can handle high volumes with minimal pressure drops, while mechanical conveyors offer better control over particle velocity and direction. Additionally, the system includes a dust collection system to capture and filter airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment. Control units monitor and adjust the system parameters in real-time, optimizing performance based on production demands.

Working Scene Characteristics: Industrial Applications
The Manganese Carbonate Powder Conveying System is widely used in various industrial applications where manganese carbonate is a critical component. One primary application is in the battery manufacturing industry, where high-purity manganese carbonate is used as an electrode material in lithium-ion batteries. The system must maintain strict purity standards, as any contamination can affect battery performance and lifespan. In this scenario, the conveying system operates under controlled conditions, with minimal exposure to moisture and other contaminants, ensuring the powder remains in its optimal state for processing. Another common application is in the chemical industry, where manganese carbonate is used as a precursor for other manganese compounds or as a catalyst in chemical reactions. Here, the system may need to handle larger volumes and operate at higher speeds to meet production throughput requirements. The characteristics of the working scene, such as the scale of production, the required purity level, and the environmental regulations, directly influence the design and configuration of the conveying system. For example, in large-scale battery manufacturing plants, the system may be integrated with automated batching and mixing equipment, requiring precise control over the flow rate and timing of the powder delivery. In smaller chemical processing facilities, the system may be simpler, focusing on efficient transport from storage to reaction vessels.
Advantages and Benefits of the System
The Manganese Carbonate Powder Conveying System offers several advantages that make it an ideal choice for handling manganese carbonate powders. One key benefit is its ability to maintain the integrity of the powder, preventing agglomeration or degradation during transport. The system’s low air velocity and gentle handling minimize particle breakage, ensuring the powder retains its desired particle size distribution. This is particularly important for manganese carbonate, as particle size affects its reactivity and performance in downstream processes. Another advantage is the system’s energy efficiency. By optimizing air flow and conveyor speed, the system reduces energy consumption compared to traditional methods like manual handling or bulk transport. This not only lowers operational costs but also contributes to environmental sustainability. The system also enhances safety in the workplace by containing dust and preventing dust explosions, which are common hazards when handling fine powders. The integration of dust collection systems and explosion-proof components ensures compliance with safety standards, reducing the risk of accidents and improving overall workplace safety. Additionally, the system’s modular design allows for easy customization and expansion, making it adaptable to changing production needs and future growth.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced Manganese Carbonate Powder Conveying Systems that address the unique challenges of handling fine powders like manganese carbonate. By combining robust engineering, efficient components, and careful design, the system ensures reliable, safe, and cost-effective material transport in various industrial applications. Whether used in battery manufacturing, chemical processing, or other industries, the system’s ability to maintain product quality, enhance operational efficiency, and ensure workplace safety makes it a valuable asset for any production facility. With its focus on innovation and customer needs, HeadPowder continues to provide solutions that meet the evolving demands of the industrial sector.